Water-based PUD adhesives are candidates for wrapping instrument panels, door panels, seat trim and headliners. Evaluate adhesion, temperature response, humid-heat durability, appearance, processing and odor/VOC for the specified grade and actual materials. A material category or country of origin does not establish the performance ranking of individual products.
RELANET develops water-based polyurethane adhesives for automotive interiors, with R-5670 and R-5610 addressing different wrapping and illuminated-trim applications. This page retains six evaluation areas and the original comparison material for preliminary review. Verify the grade, sample, method and original report behind each figure before use; the material does not establish whole-range performance, competitor rankings or project guarantees.
Preface: industry test framework
The original material refers to GB/T 2792-2014 peel testing, ASTM D412 tensile testing, humid-heat exposure at 60°C/95% RH and cycling from -40°C to 105°C. These are separate methods or conditions whose applicability and records must be checked individually. Use the customer-specified NES M0160 for odor; confirm VOC, cabin air quality and regulations separately. Use the following comparisons only after their complete test basis has been verified.
Competitor A; Competitor B; a benchmark PUD; and imported Competitor C. The competitor identities are anonymized in the source manuscript.
RELANET test sample: R-5670 interior PUD, described as the principal commercial model. All samples were crosslinked for 24 hours at 23°C with the same 100:5 ratio of water-dispersible isocyanate hardener. The chart descriptions below correspond to the figures in the original manuscript.
Advantage 1: high bond strength and leading multi-substrate adhesion to reduce edge lift and debonding
Door-panel folds, instrument-panel curves and seat coverings require peel and durability methods suited to their loads. The grade, backing and surface condition of PP, TPO and leather affect the interface. A single 180° peel result cannot predict installed service life.
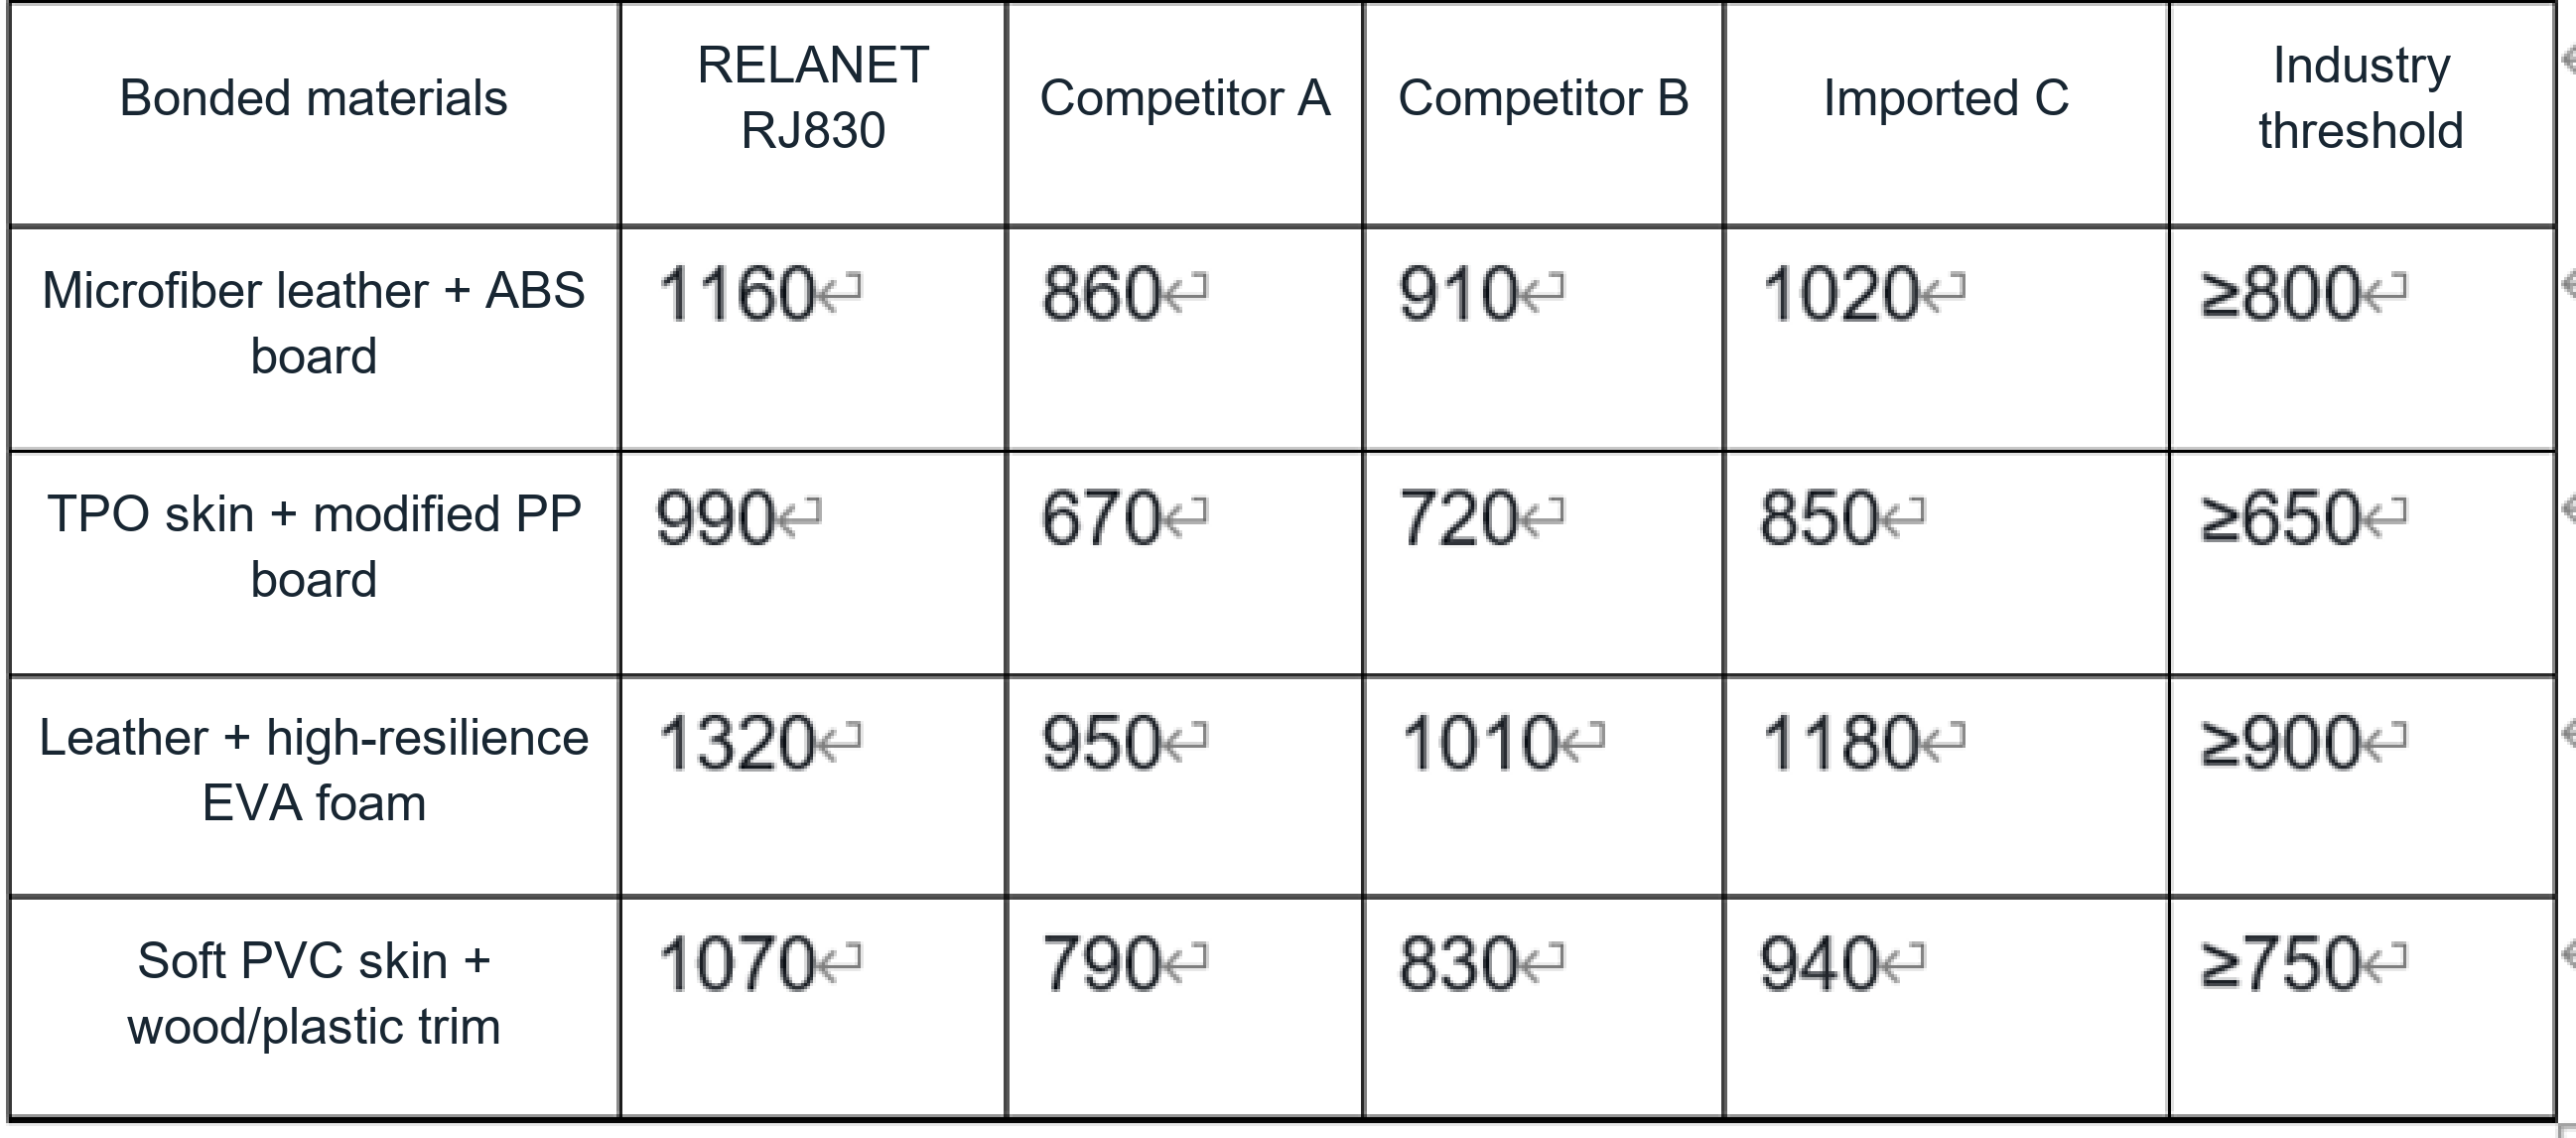
Measured comparison data (N/m, 180° peel strength)
Table. Adhesion of four product groups
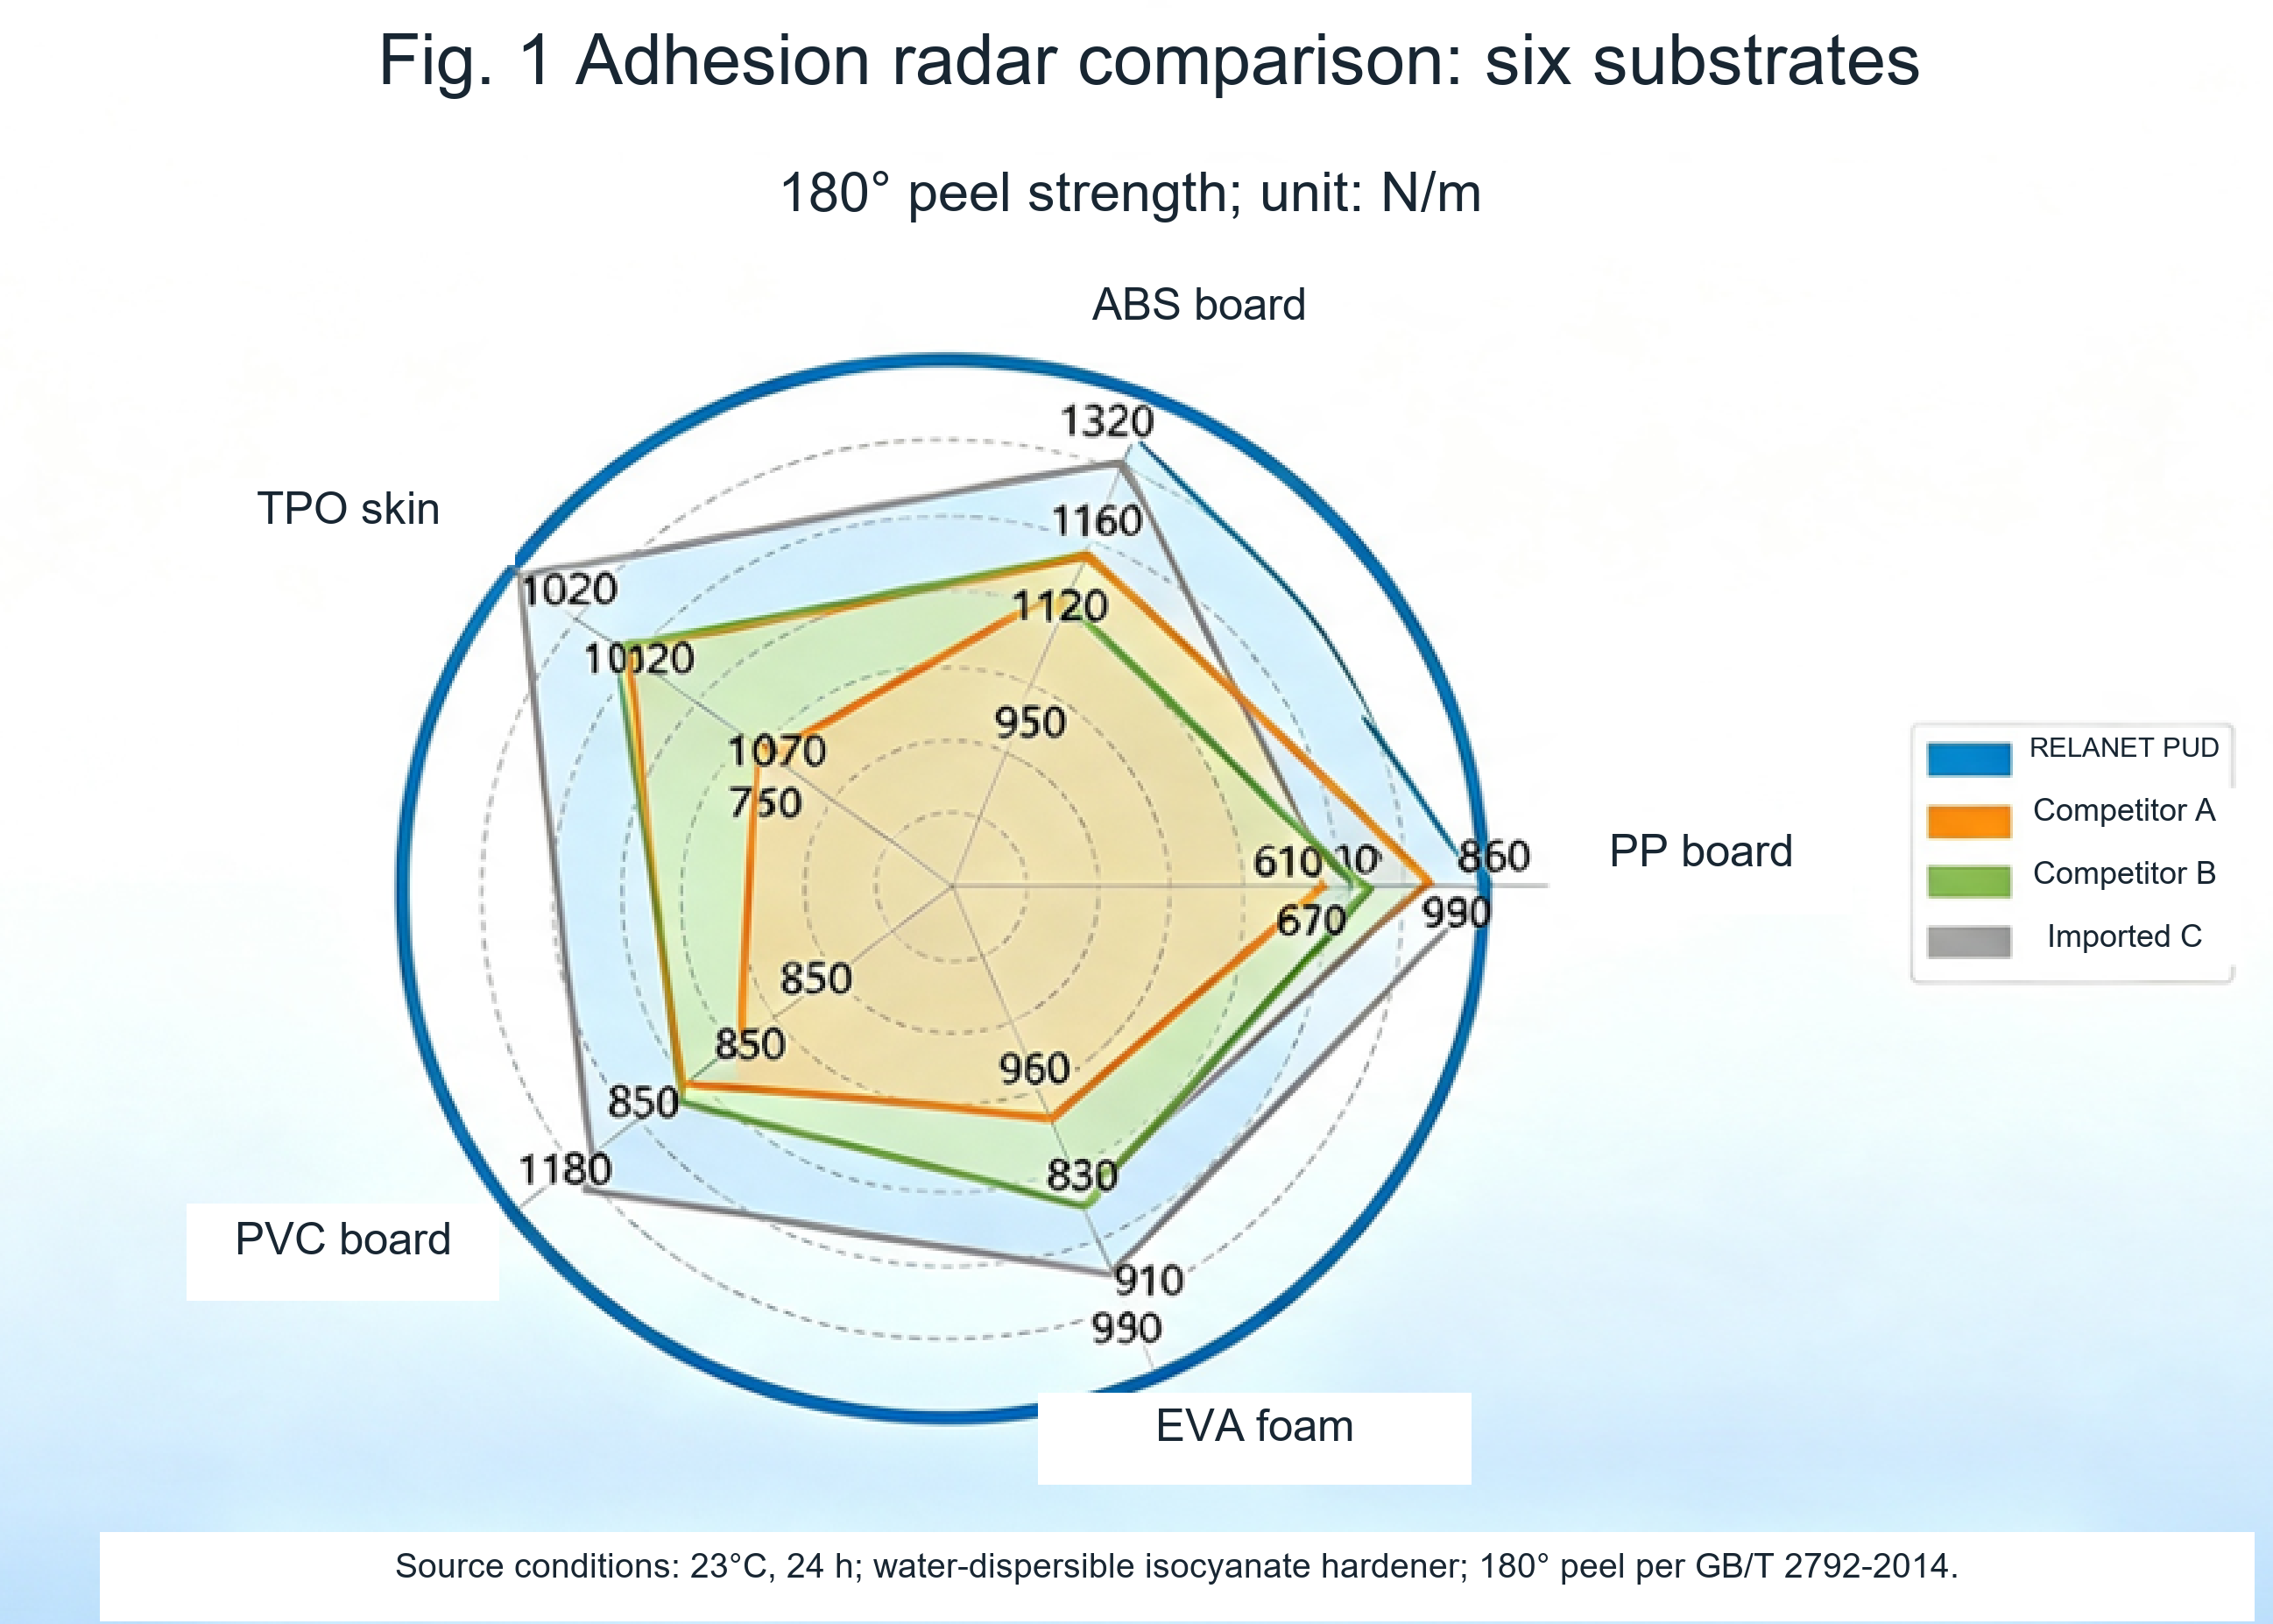
The diagram covers ABS, PP, leather, foam, PVC and TPO. Verify the units, samples, pretreatment and original reports for each axis before comparing results; the figure does not establish universal substrate compatibility or a product ranking.
Interpretation
Molecular design alone does not establish that a PUD can bond PP or TPO without pretreatment. Evaluate cleaning, primer or activation for each grade, and follow R-5610 technical requirements for PP and IXPP. R-7206 and R-7110 belong to a separate modified-polyolefin hot-melt system and can omit primer, flame or plasma on confirmed PP grades, clean surfaces and validated processes. Verify the original cost, peel and cycling records separately; they must not be transferred to the entire PUD range.
Advantage 2: broad temperature stability from -40°C to 105°C for severe climates
Vehicle cabins experience a very wide thermal range: temperatures can fall to -30°C or -40°C in northern winters, while a closed cabin exposed to summer sun can exceed 100°C. Conventional PUDs may harden and crack at low temperature or soften and become tacky at high temperature. RELANET adjusts the glass-transition behavior of the adhesive film to create a broad operating-temperature range.
Peel-strength retention across the temperature gradient
- 1. After 24 hours at -40°C, peel-strength retention was reported as 92% for RELANET, 71% for Competitor A, 76% for Competitor B and 83% for imported Competitor C.
- 2. After 24 hours at 105°C, peel-strength retention was reported as 88% for RELANET, 66% for Competitor A, 70% for Competitor B and 79% for Competitor C.
- 3. After 100 thermal cycles between -40°C and 105°C, the RELANET sample showed no delamination and retained 85% of its strength. The three comparison products showed localized edge lift and retained 58%-72%.
Figure 2. Peel-strength retention across the full temperature range
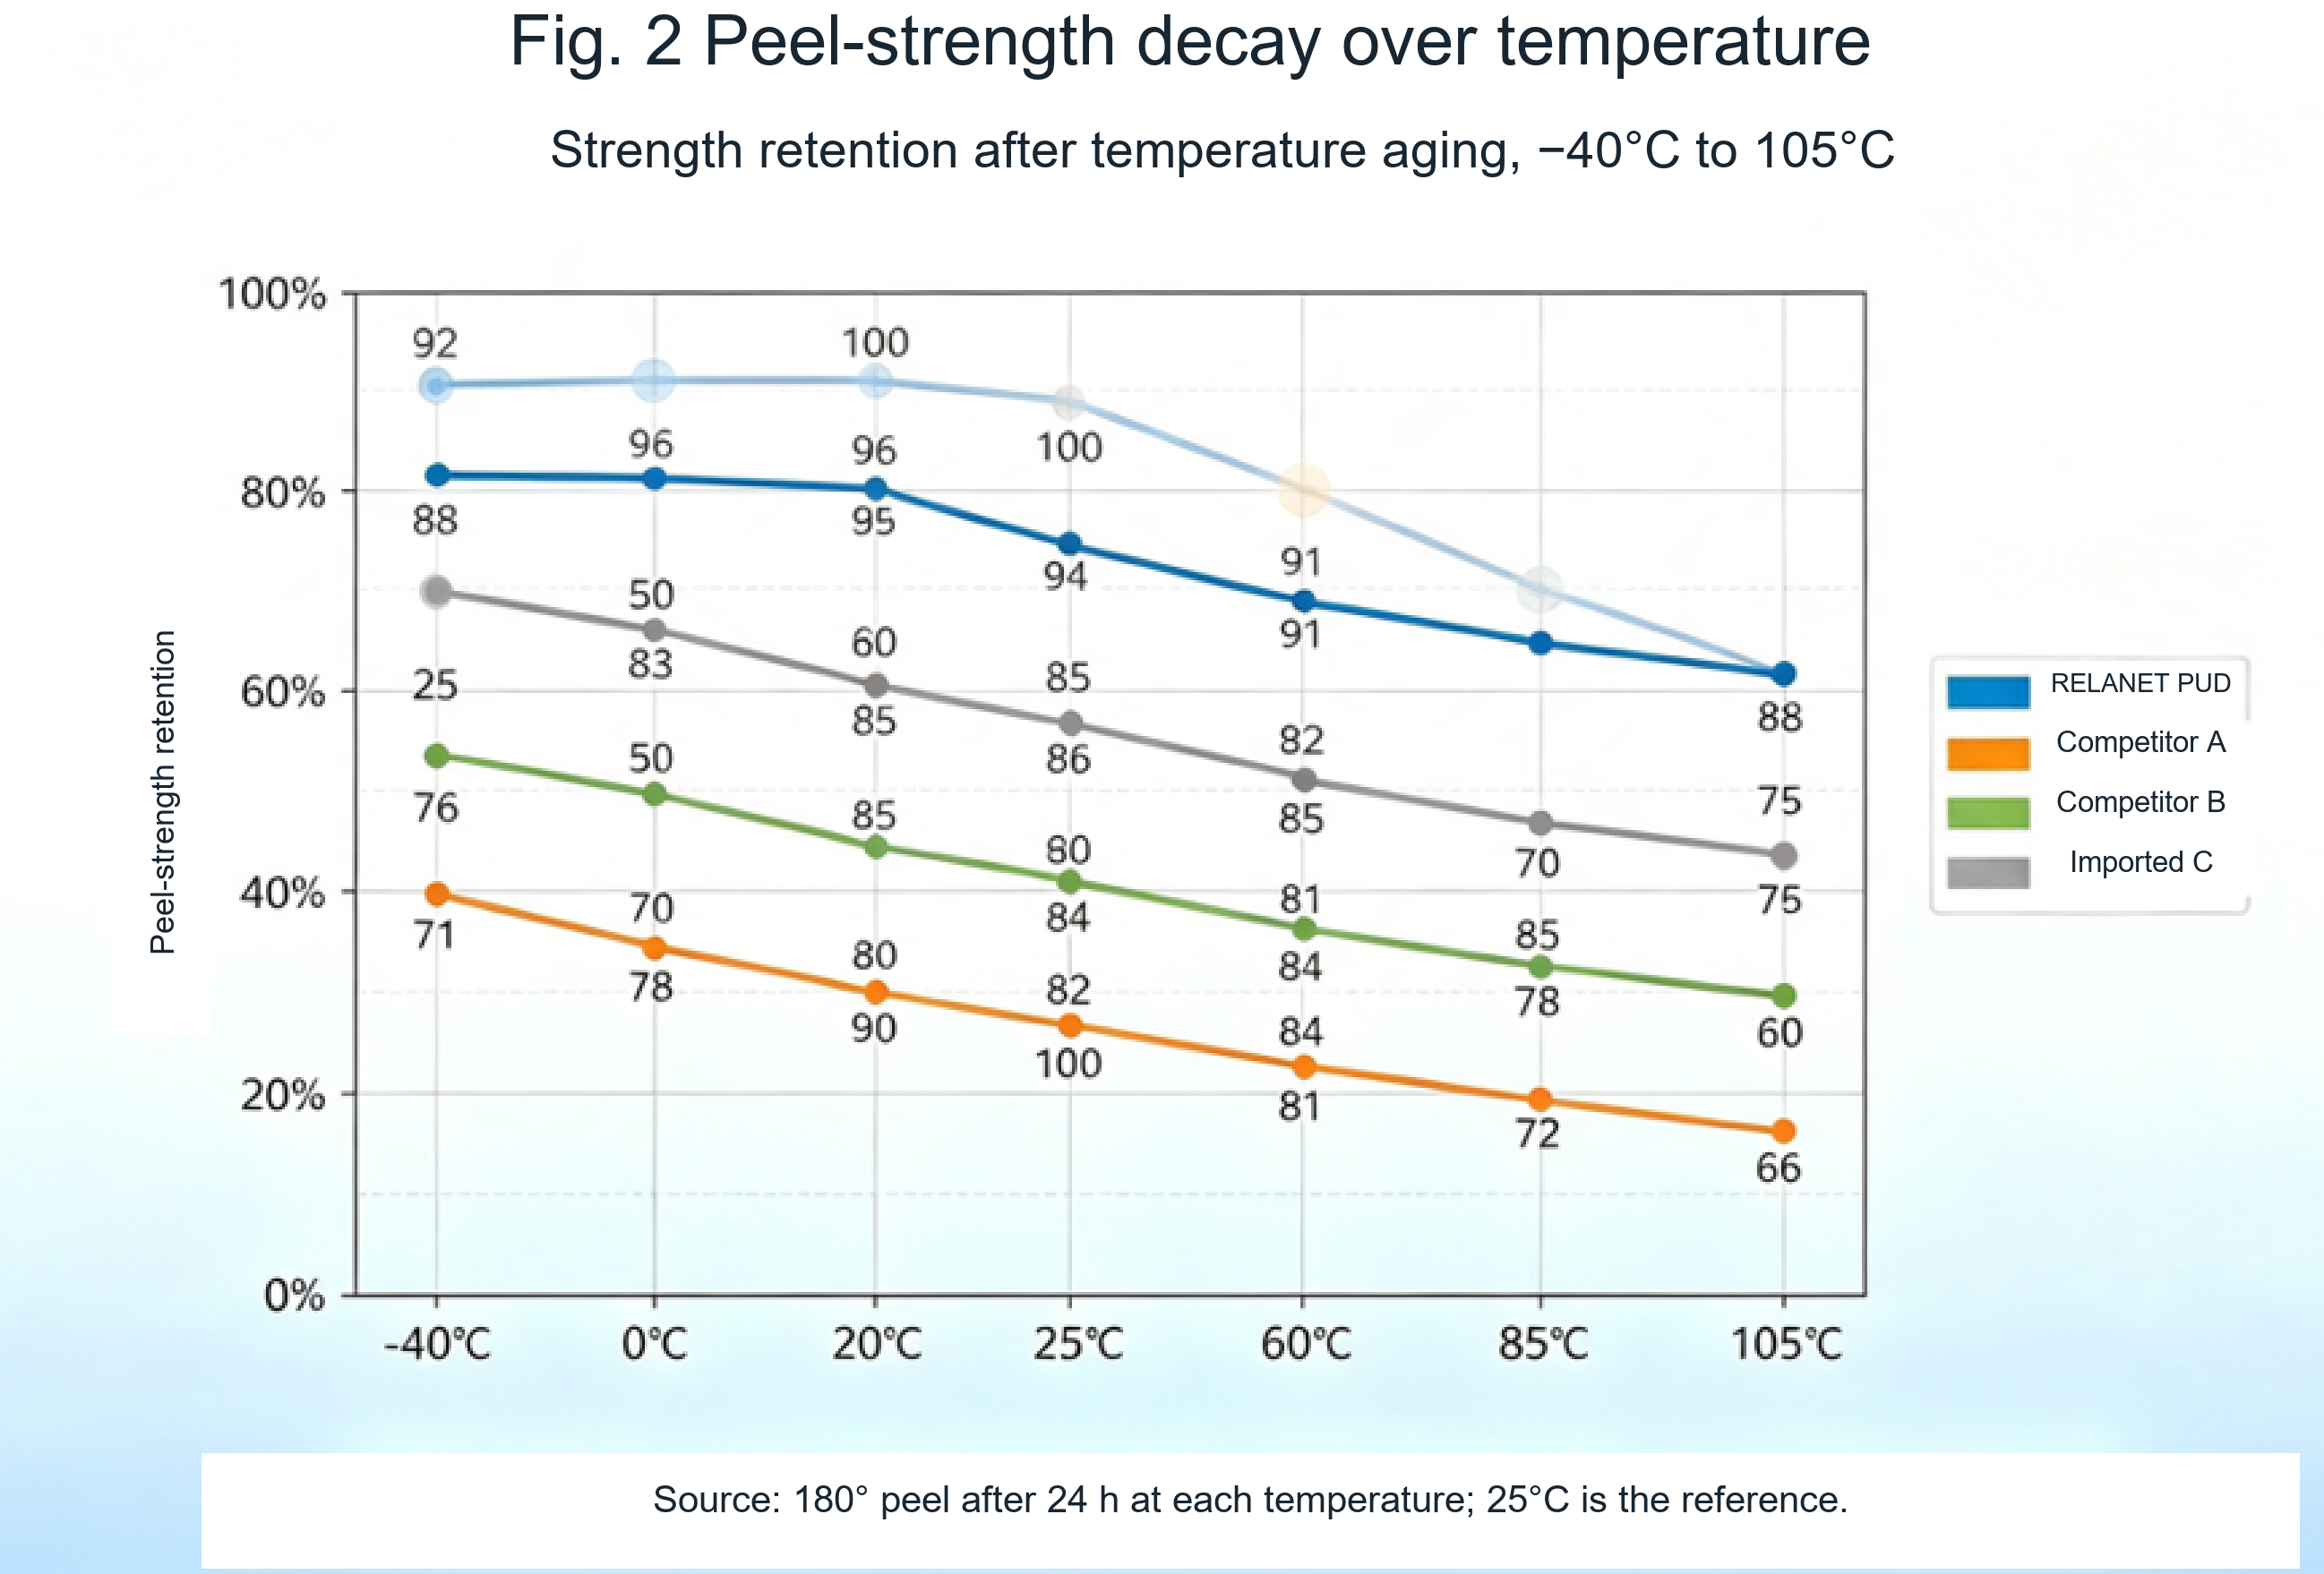
Figure description: temperature appears on the horizontal axis and peel strength on the vertical axis. The blue RELANET curve declines gradually; the curves for Competitors A and B fall sharply at low temperature, while imported Competitor C declines more at high temperature.
Interpretation
The RELANET film has a reported elongation at break of up to 850% at room temperature and retains 500%-800% elongation at 10°C, compared with 300%-500% for the comparison set. This flexibility helps prevent leather tearing during manual wrapping in cold workshops and reduces cracking in severe winter use. During summer heat exposure, the adhesive layer is designed not to flow or bleed oil into the skin. The manuscript cites series-production applications in both cold northeastern and hot Hainan-region vehicle programs as evidence of broad climate coverage.
Advantage 3: 1,000-hour humid-heat and hydrolysis resistance to reduce long-term blistering
Relative humidity in South China and coastal areas can remain above 85% for long periods. Moisture can gradually penetrate the bond line, causing hydrolysis, whitening, swelling and debonding. This is described as a common cause of concentrated interior aging after three to five years in coastal service. Whereas the industry often uses a 500-hour hydrolysis test, the RELANET manuscript reports a 1,000-hour aging program.
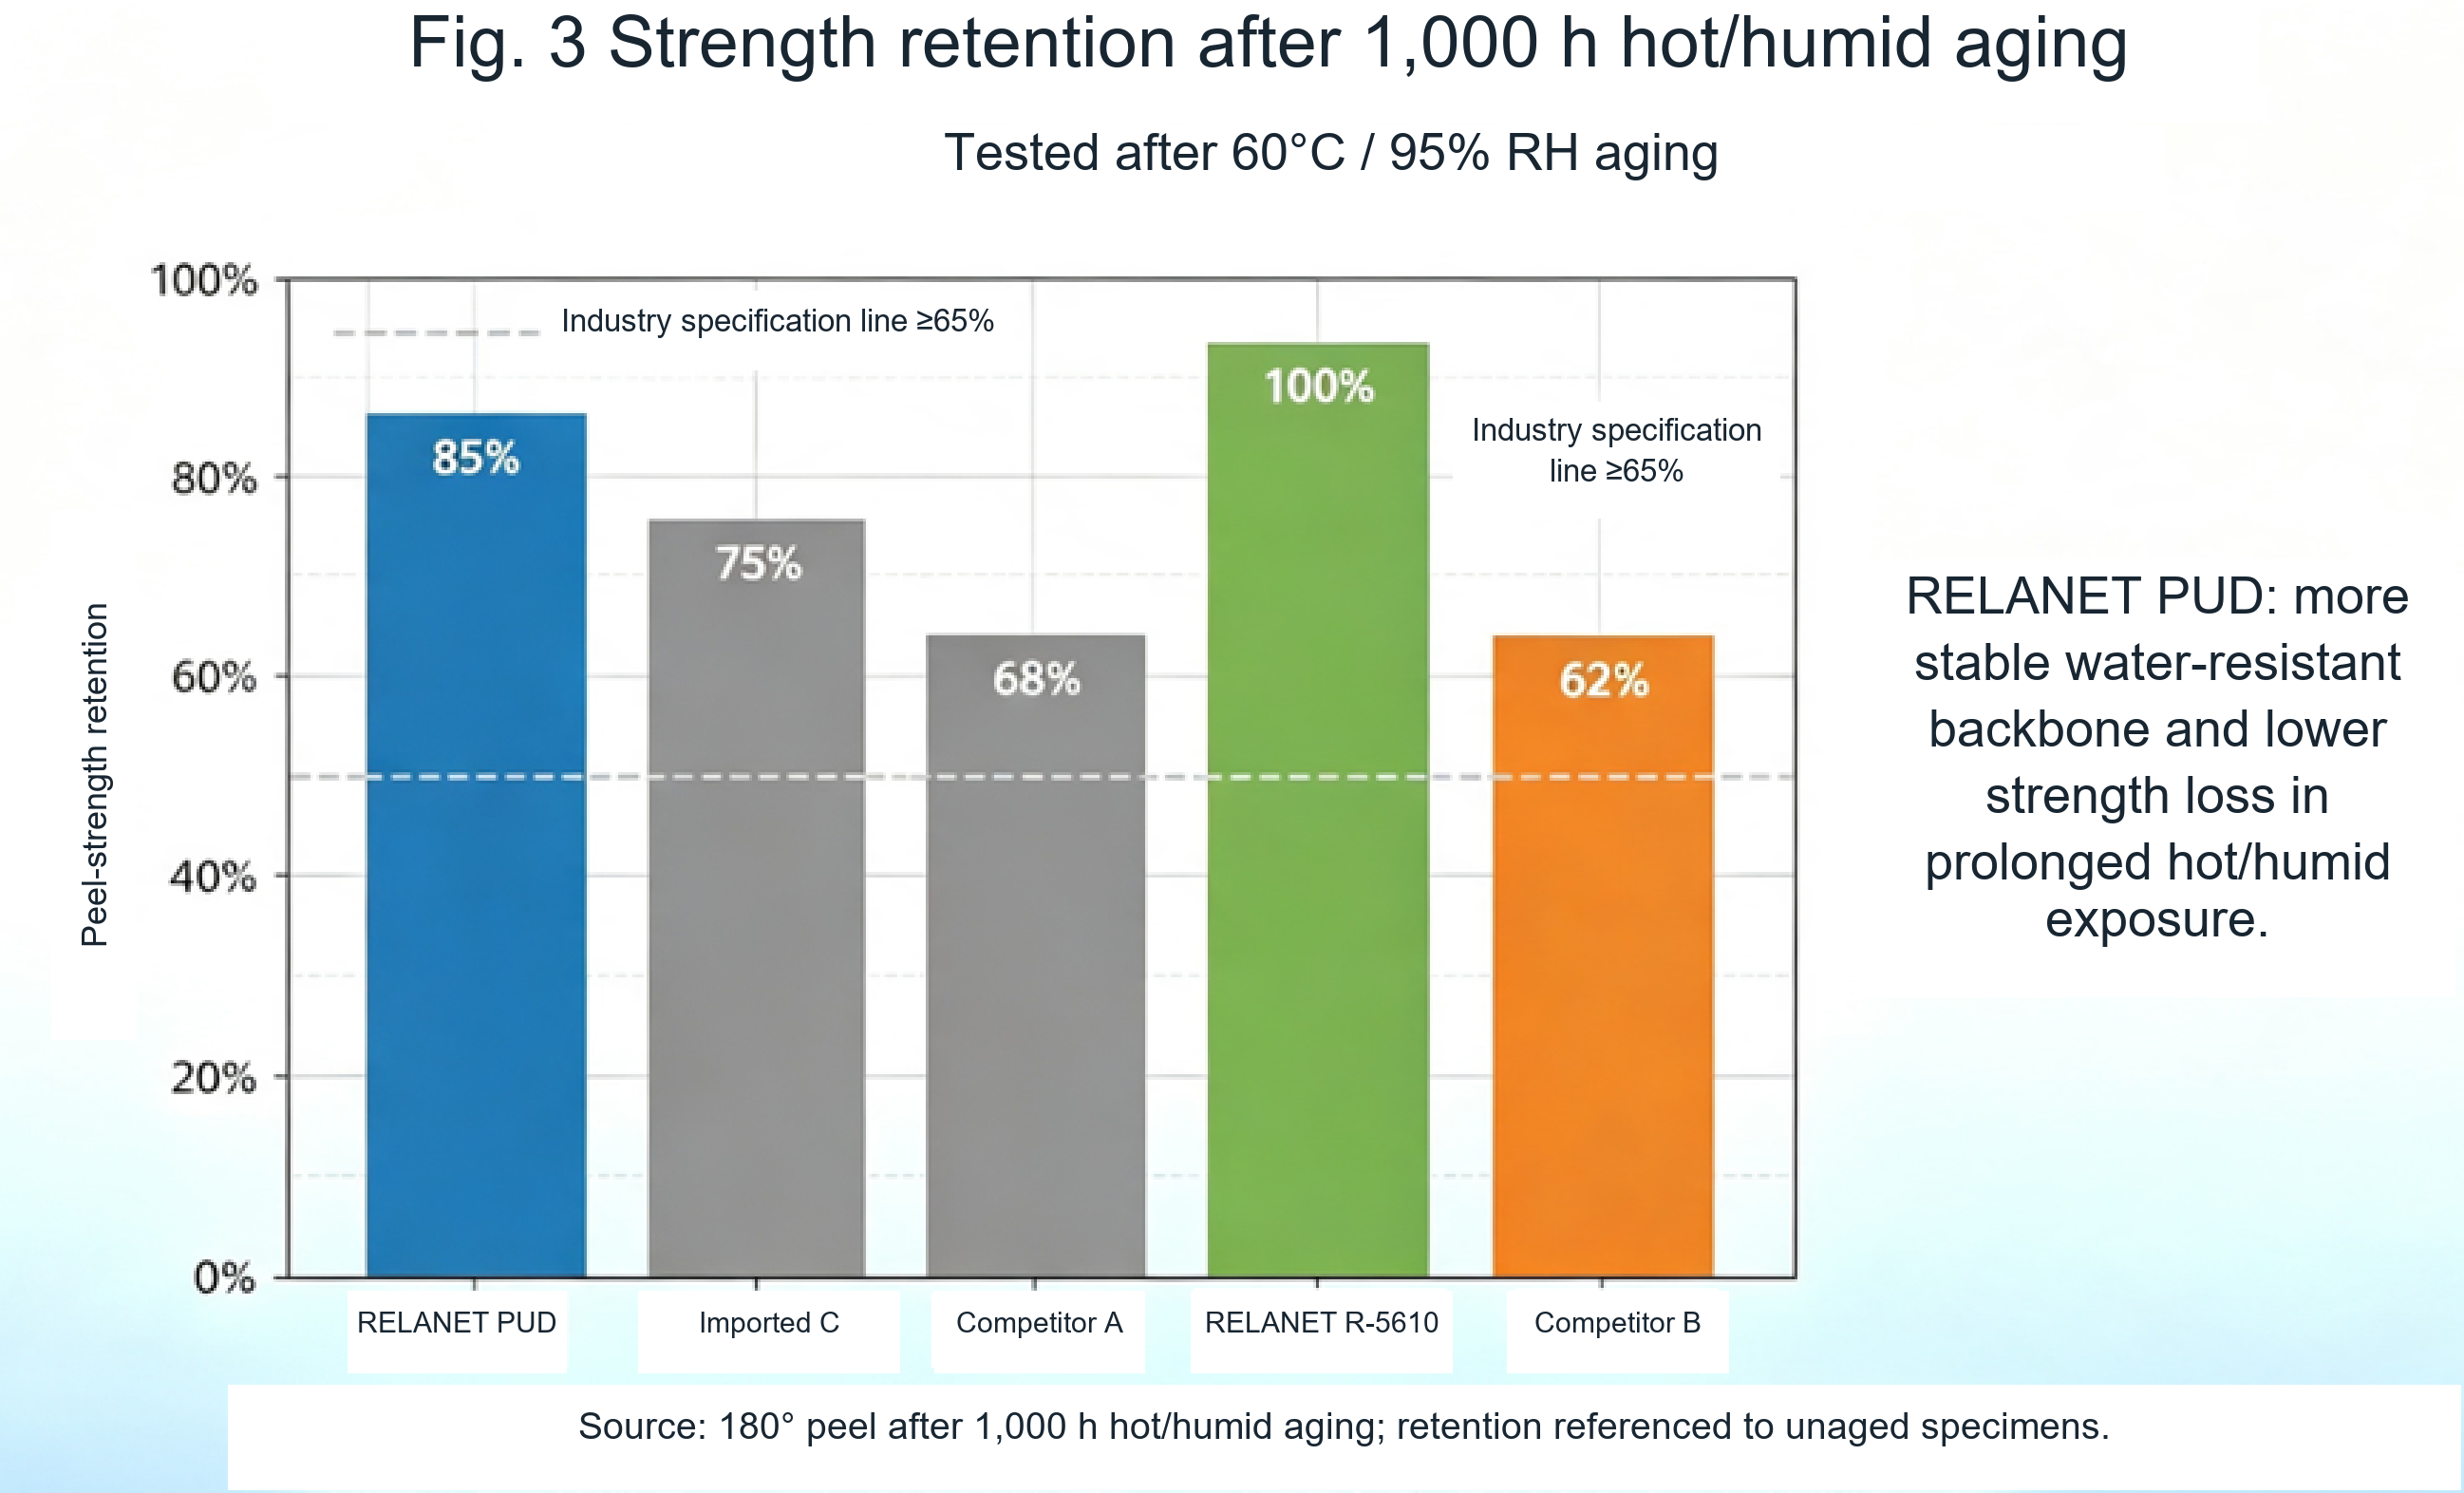
Measured aging at 60°C and 95% RH for 1,000 hours
- RELANET R-5670: the film remained clear, without whitening or swelling, and retained 85% of peel strength.
- Competitor A PUD: localized film whitening and 62% retained strength.
- Competitor B PUD: slight hydrolysis and 68% retained strength.
- Competitor C PUD: slight whitening and 75% retained strength.
The manuscript cites ≥65% retention as a commonly applied higher-level industry requirement.
Figure 3. Strength retention after 1,000 hours of humid-heat aging
Interpretation
RELANET uses a hydrolysis-resistant polycarbonate backbone in place of conventional polyester segments that are more susceptible to hydrolysis, making it harder for water molecules to disrupt the polyurethane chain. Production feedback cited from retrofit suppliers in the Pearl River Delta and coastal Fujian reports that wrapped interiors remained flat and secure after five years, without moisture-related blistering or detachment. The manuscript describes a service-life improvement of more than 40% over the comparison products and a corresponding reduction in after-sales maintenance cost.
Evaluation 4: chemical, UV and yellowing resistance
White, cream and light-grey interiors are increasingly common in new-energy vehicles. Aromatic PUDs can yellow under ultraviolet exposure. Neutral cleaners, hand cream and leather-care products can also contact the adhesive layer and cause swelling or debonding, creating two long-standing design concerns.
Two dedicated test groups
- 1. Chemical-resistance test: 72-hour exposure to a neutral interior cleaner and silicone-oil care fluid.
RELANET: no swelling and less than 6% strength loss; Competitor A: 21% loss; Competitor B: 17% loss; imported Competitor C: 11% loss.
- 2. Yellowing-resistance test: 500 hours at 85°C plus 300 hours of ultraviolet aging.
RELANET: color difference ΔE <1.2, with no yellowing visible to the unaided eye.
Competitors A and B: ΔE >3.8, with obvious yellowing; imported Competitor C: ΔE ≈2.1, with slight yellowing.
Figure 4. Color-block comparison after yellowing exposure
Interpretation
An aliphatic structure can reduce yellowing tendency, but does not guarantee permanent color stability across all PUD grades or complete interior parts. Evaluate color change, cleaner contact, silicone oil and plasticizer migration separately for leather, TPO, microfiber and PVC, recording adhesive thickness, exposure, temperature, duration and failure mode.
Advantage 5: production-friendly processing, wider tolerance and lower manufacturing cost
Even an adhesive with strong laboratory performance cannot succeed if it is incompatible with the production line. RELANET separately optimizes materials for manual and automated wrapping to address narrow activation windows, unsuitable open times, high drying energy and excessive scrap. The following figures compare process parameters.
Table. Process-data comparison
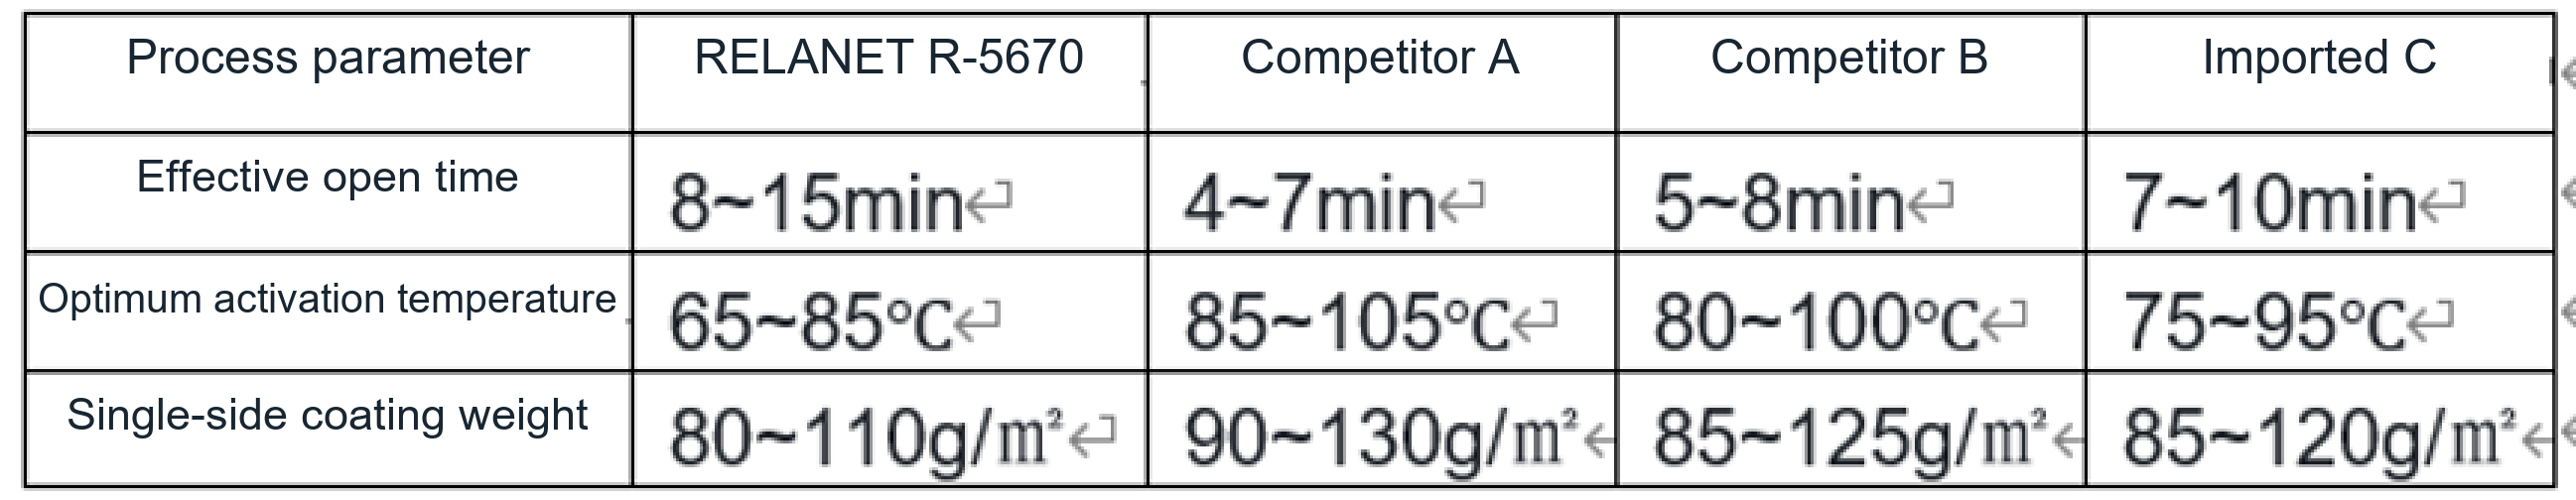
Figure 5. Activation-temperature and open-time operating window
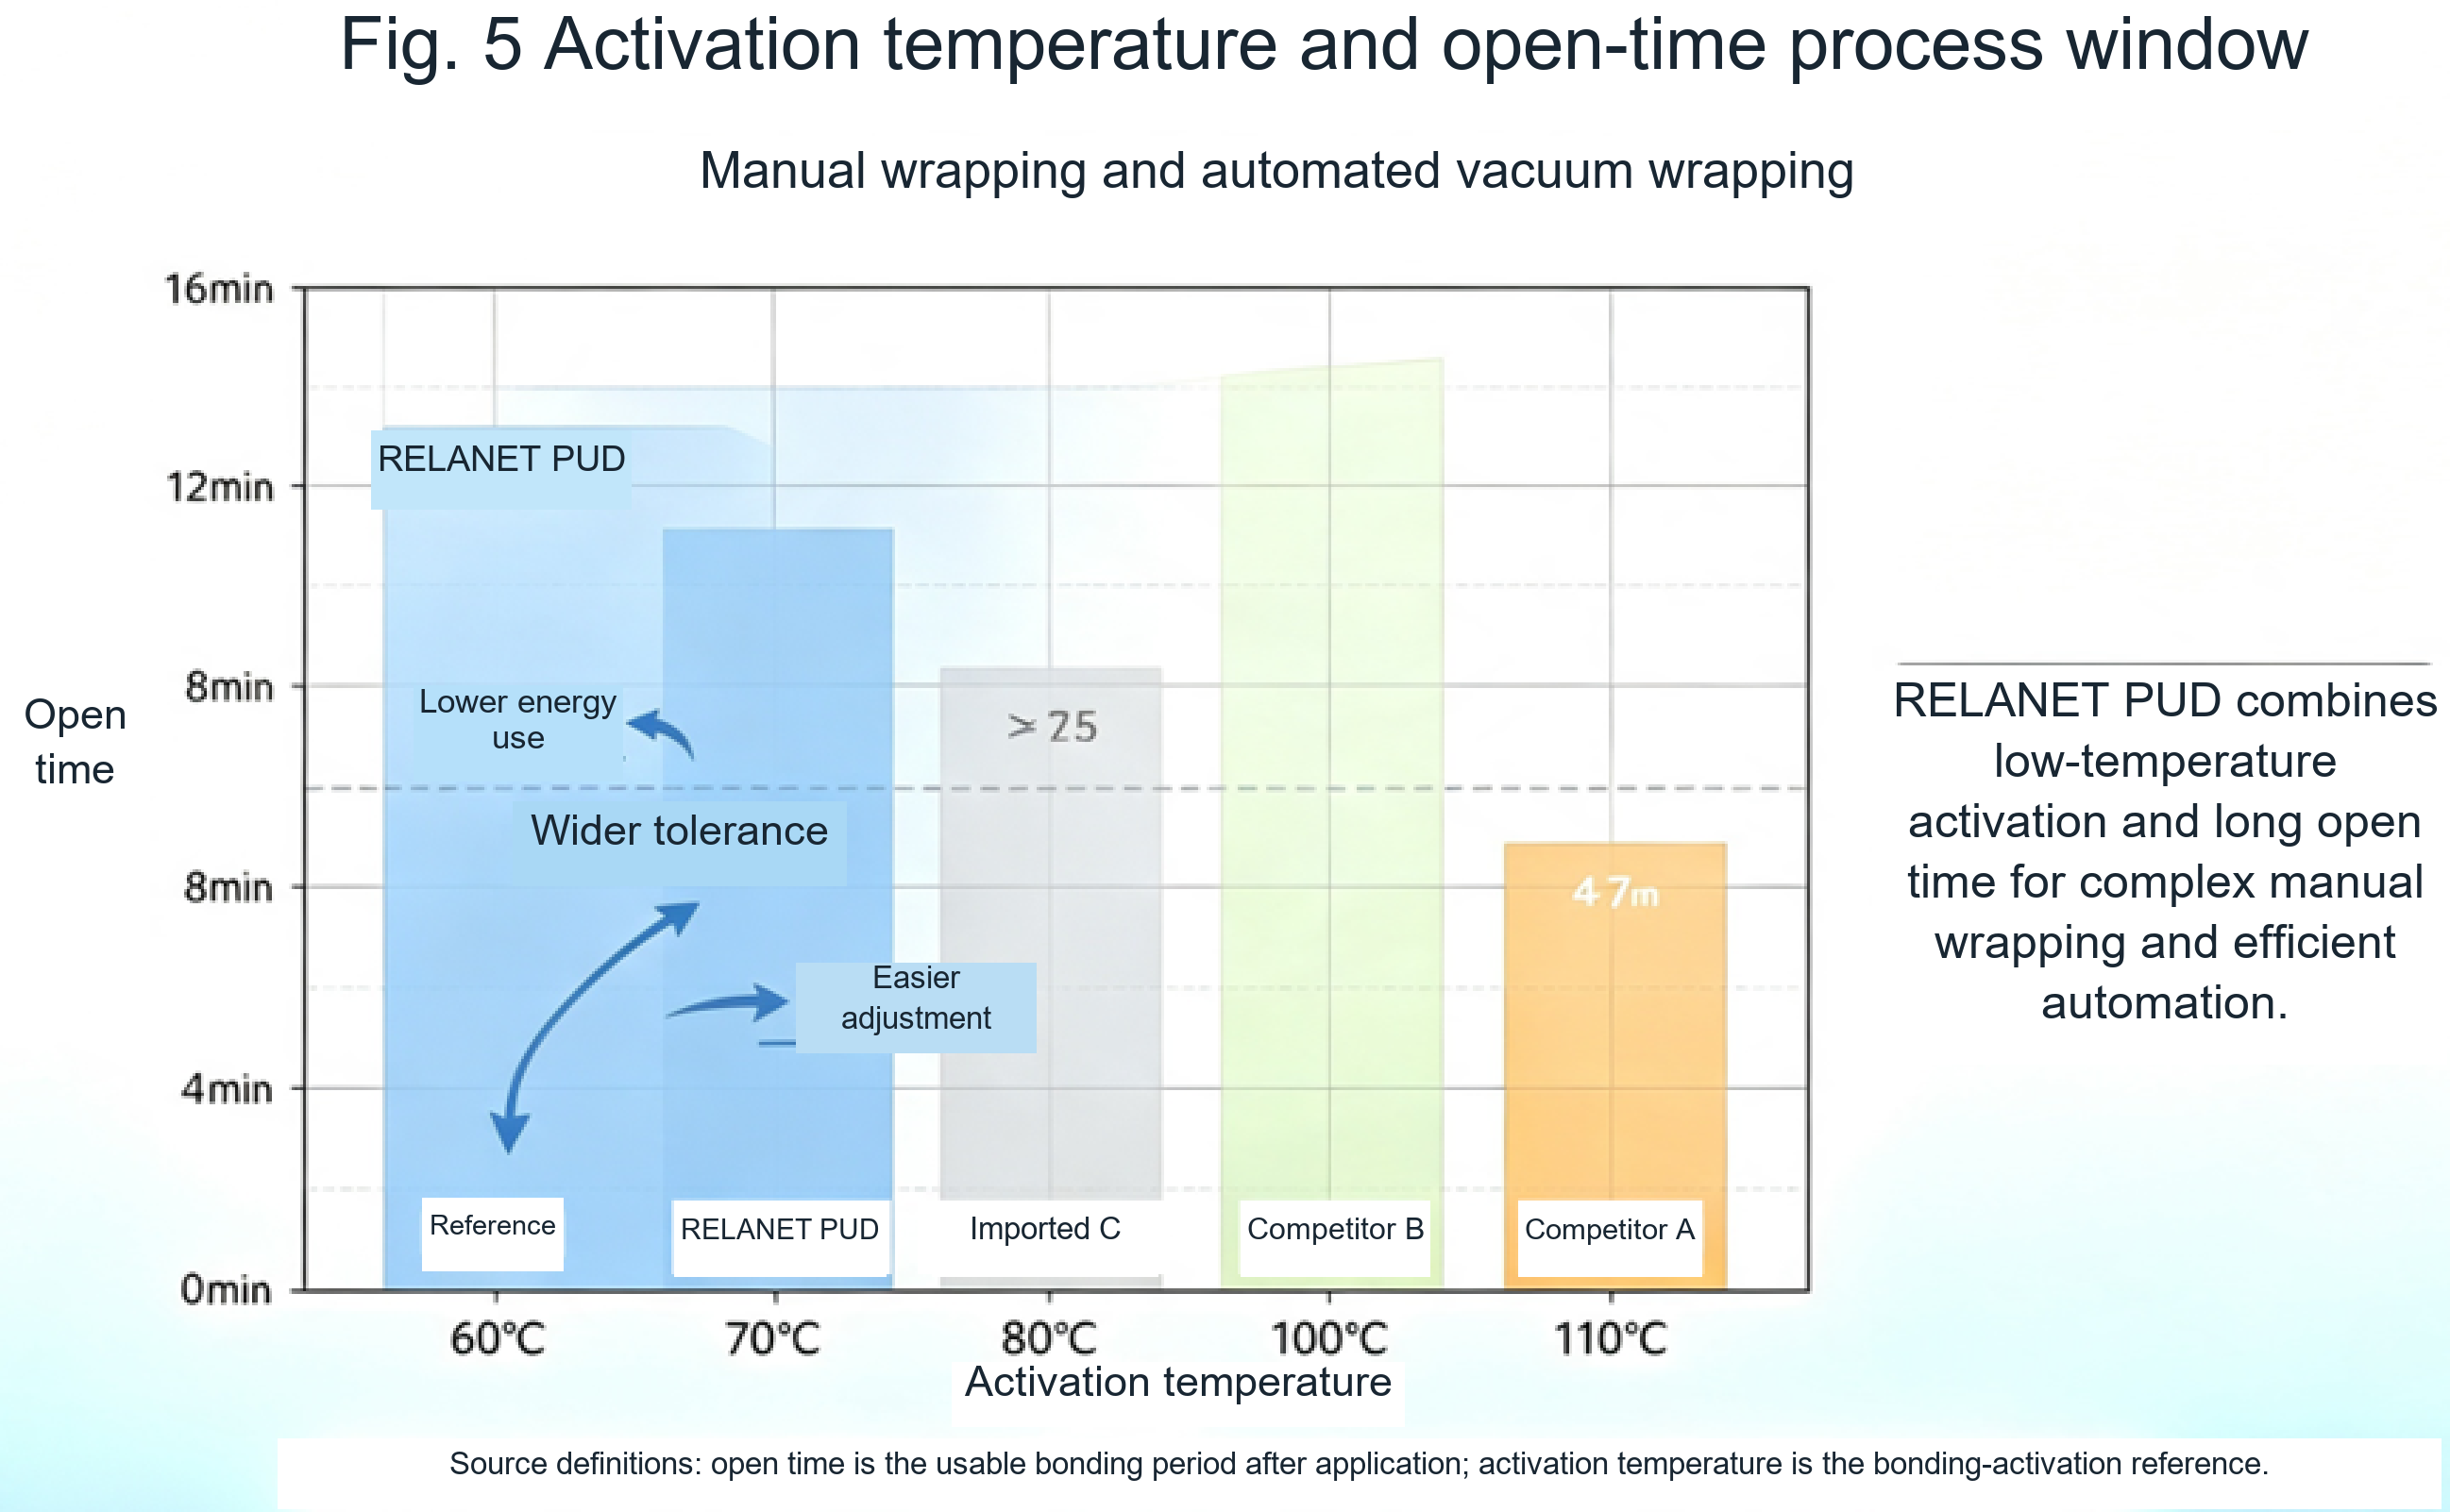
Figure description: the RELANET operating region is wider than the comparison regions, indicating greater process tolerance.
Interpretation
- 1. Manual wrapping: an 8-15 minute open time allows slow skin adjustment over curved surfaces and irregular corners. After adoption in a South China winter workshop, the reported scrap rate among newly trained operators fell by 60%.
- 2. Automated production: activation from 65°C was reported to reduce oven energy by 20%. Thin leather and light-colored skins are less likely to shrink at this temperature, and a 3-8 minute drying time can align with the line cycle.
- 3. Material efficiency: lower coat weight reduces material use by 10%-20% per square metre in the stated comparison, lowering procurement cost at scale. The dried film is transparent and does not obscure the leather grain, supporting interior appearance.
Evaluation 6: odor, VOC and regulatory requirements
Use the customer-specified NES M0160 for odor assessment. Confirm VOC methods and targets separately; Nissan projects may involve NES M0402 and NES M0403. GB/T 27630 concerns passenger-vehicle cabin air quality and is not a single adhesive VOC limit. Verify REACH, ELV and durability requirements independently. Naming a standard does not establish a test pass or regulatory approval.
Table. VOC comparison
Figure 6. Bar chart comparing VOC release
Figure description: the national-standard limit is marked in red, and the reported RELANET value is below both the limit and the comparison products.
Interpretation
Water-based formulation can reduce reliance on organic solvents, but odor, VOC, restricted substances and safety classification require the specific grade's SDS and valid test information. Assess ventilation, exhaust treatment and fire protection for the complete production line. A water-based system does not establish zero emissions, an odor-free cabin or an exemption from protective facilities. Customer applications and export suitability require authorized project and compliance records.
Conclusion: the combined value of RELANET PUD and a new benchmark for domestic interior adhesives
The six evaluation areas should form one part-specific validation record: initial bonding, temperature and humid-heat durability, appearance stability, process window and odor/VOC. Results collectively support selection; one passed test does not establish all properties, service life or a fixed cost saving.
RELANET can support adhesive selection, process tuning and aging evaluation for specified constructions such as PP/glass-fiber carriers and ultrathin leather. Compare candidates using equivalent specimens and conditions; unverified charts or isolated results do not establish overall superiority to another brand.
RELANET will continue to focus on water-based polyurethane for automotive interiors, supporting the transition to water-based processes through material technology, stable products and rapid localized technical service. The goal is to work with automakers and interior suppliers to advance domestically developed automotive bonding materials.
Separate odor, VOC and durability validation
NES M0160 addresses odor testing of automotive interior parts. It does not replace VOC, vehicle-cabin air-quality, durability or regulatory assessment. Confirm the revision, sample, conditions and targets for the customer project; naming a standard does not establish a pass.
- Use the customer-specified NES M0160 revision and odor test conditions. Any stated grade requires a valid report for the corresponding sample.
- Confirm VOC methods and targets separately; Nissan projects may involve NES M0402 and NES M0403. GB/T 27630 concerns passenger-vehicle cabin air quality and is not a single adhesive VOC limit. Check REACH, ELV and durability requirements separately.
Sources and validation basis Nissan · NES M0160 / NES M0402 / NES M0403
R-7206 / R-7110: conditions for bonding PP without activation
R-7206 and R-7110 are modified polyolefin hot-melt adhesives. Compatibility between the non-polar polyolefin and PP systems helps explain direct bonding on confirmed PP grades, clean surfaces and validated processes, without primer, flame or plasma pretreatment.
Omitting activation does not remove the need for cleaning. Control release agents, oil, dust, recycled content and surface condition, then validate peel, heat creep and aged durability on actual parts. This does not cover every PP grade or load, and must not be generalized to all PUD adhesives.