1. Company introduction: RELANET
As China's automotive industry moves toward electrification, lightweight construction and greener manufacturing, cabin environmental quality, interior durability and production cost reduction have become central requirements for automakers and interior suppliers. As a wrapping and lamination material, the adhesive directly affects cabin air quality, product service life and line efficiency. RELANET has worked for many years in water-based polymeric bonding materials for automotive interiors. The company develops, manufactures and sells water-based polyurethane dispersions (PUDs), matching hardeners and complete application solutions, with an R&D focus on molecular modification for this specialized market.
RELANET works in the South China automotive supply region on formulation development, substrate sampling, process matching and quality validation. Assess odor using the customer-specified NES M0160 and confirm VOC, cabin air quality, durability and REACH-related requirements separately. Laboratory capabilities, equipment and credentials should be supported by available records; material-sample testing does not establish whole-vehicle or whole-range approval.
For R&D, RELANET has formed a dedicated team of polymer-material, automotive-process and interior-application engineers. Rather than relying on simple blending of general-purpose PUDs, the team follows a customized molecular-chain modification route. It targets five common weaknesses of conventional water-based adhesives: cracking during cold wrapping, debonding after high-temperature exposure, poor compatibility across substrates, excessive residual VOC and a narrow activation window on automated lines. The polyester/polycarbonate-modified PUD system has been iterated into dozens of products for manual wrapping, vacuum forming and fully automated wrapping, serving interior bonding in combustion-engine vehicles, new-energy passenger vehicles, commercial vehicles and recreational vehicles.
RELANET's service model combines product, process and customization. Before a sale, it provides substrate-bonding samples and production-line evaluation. During implementation, technical engineers tune spraying, roller coating and knife coating at the customer's site. Afterward, the team supports high/low-temperature aging, humid-heat cycling and third-party VOC testing. For new vehicle programs, customized samples for low-surface-energy PP, rigid TPO and ultrathin microfiber can be prepared within seven working days, shortening component validation. The manuscript states that products are supplied to dozens of Tier 1 interior companies for instrument panels, door trim, seats, headliners, armrests and luggage-compartment boards. Stable performance, low odor and process versatility support the industry's transition to water-based adhesives.
Looking ahead, RELANET is developing bio-based, lower-carbon PUD and ammonia-free, low-odor modified systems. Its R&D direction-lower-emission bonding, long-term durability and efficient production-is intended to help automotive interiors replace high-VOC solvent-borne adhesive and move toward greener manufacturing.
RELANET PUD applications across the complete vehicle cabin
2. RELANET PUD products for automotive interior bonding
A water-based PUD is a polyurethane dispersion used in formulation; select the finished adhesive, matching hardener and process by its confirmed grade and latest TDS. Confirm R-5670 and R-5610 applications and parameters separately instead of relying on unconfirmed historical model designations. PU leather, PVC, TPO, leather, microfiber, PP/ABS, EVA and nonwovens each require substrate and interface evaluation. One formulation is not automatically universal or free of pretreatment requirements.
(1) Basic physical and chemical properties
The basic parameters of the two products were measured under standardized laboratory conditions and are shown in the following source figure:
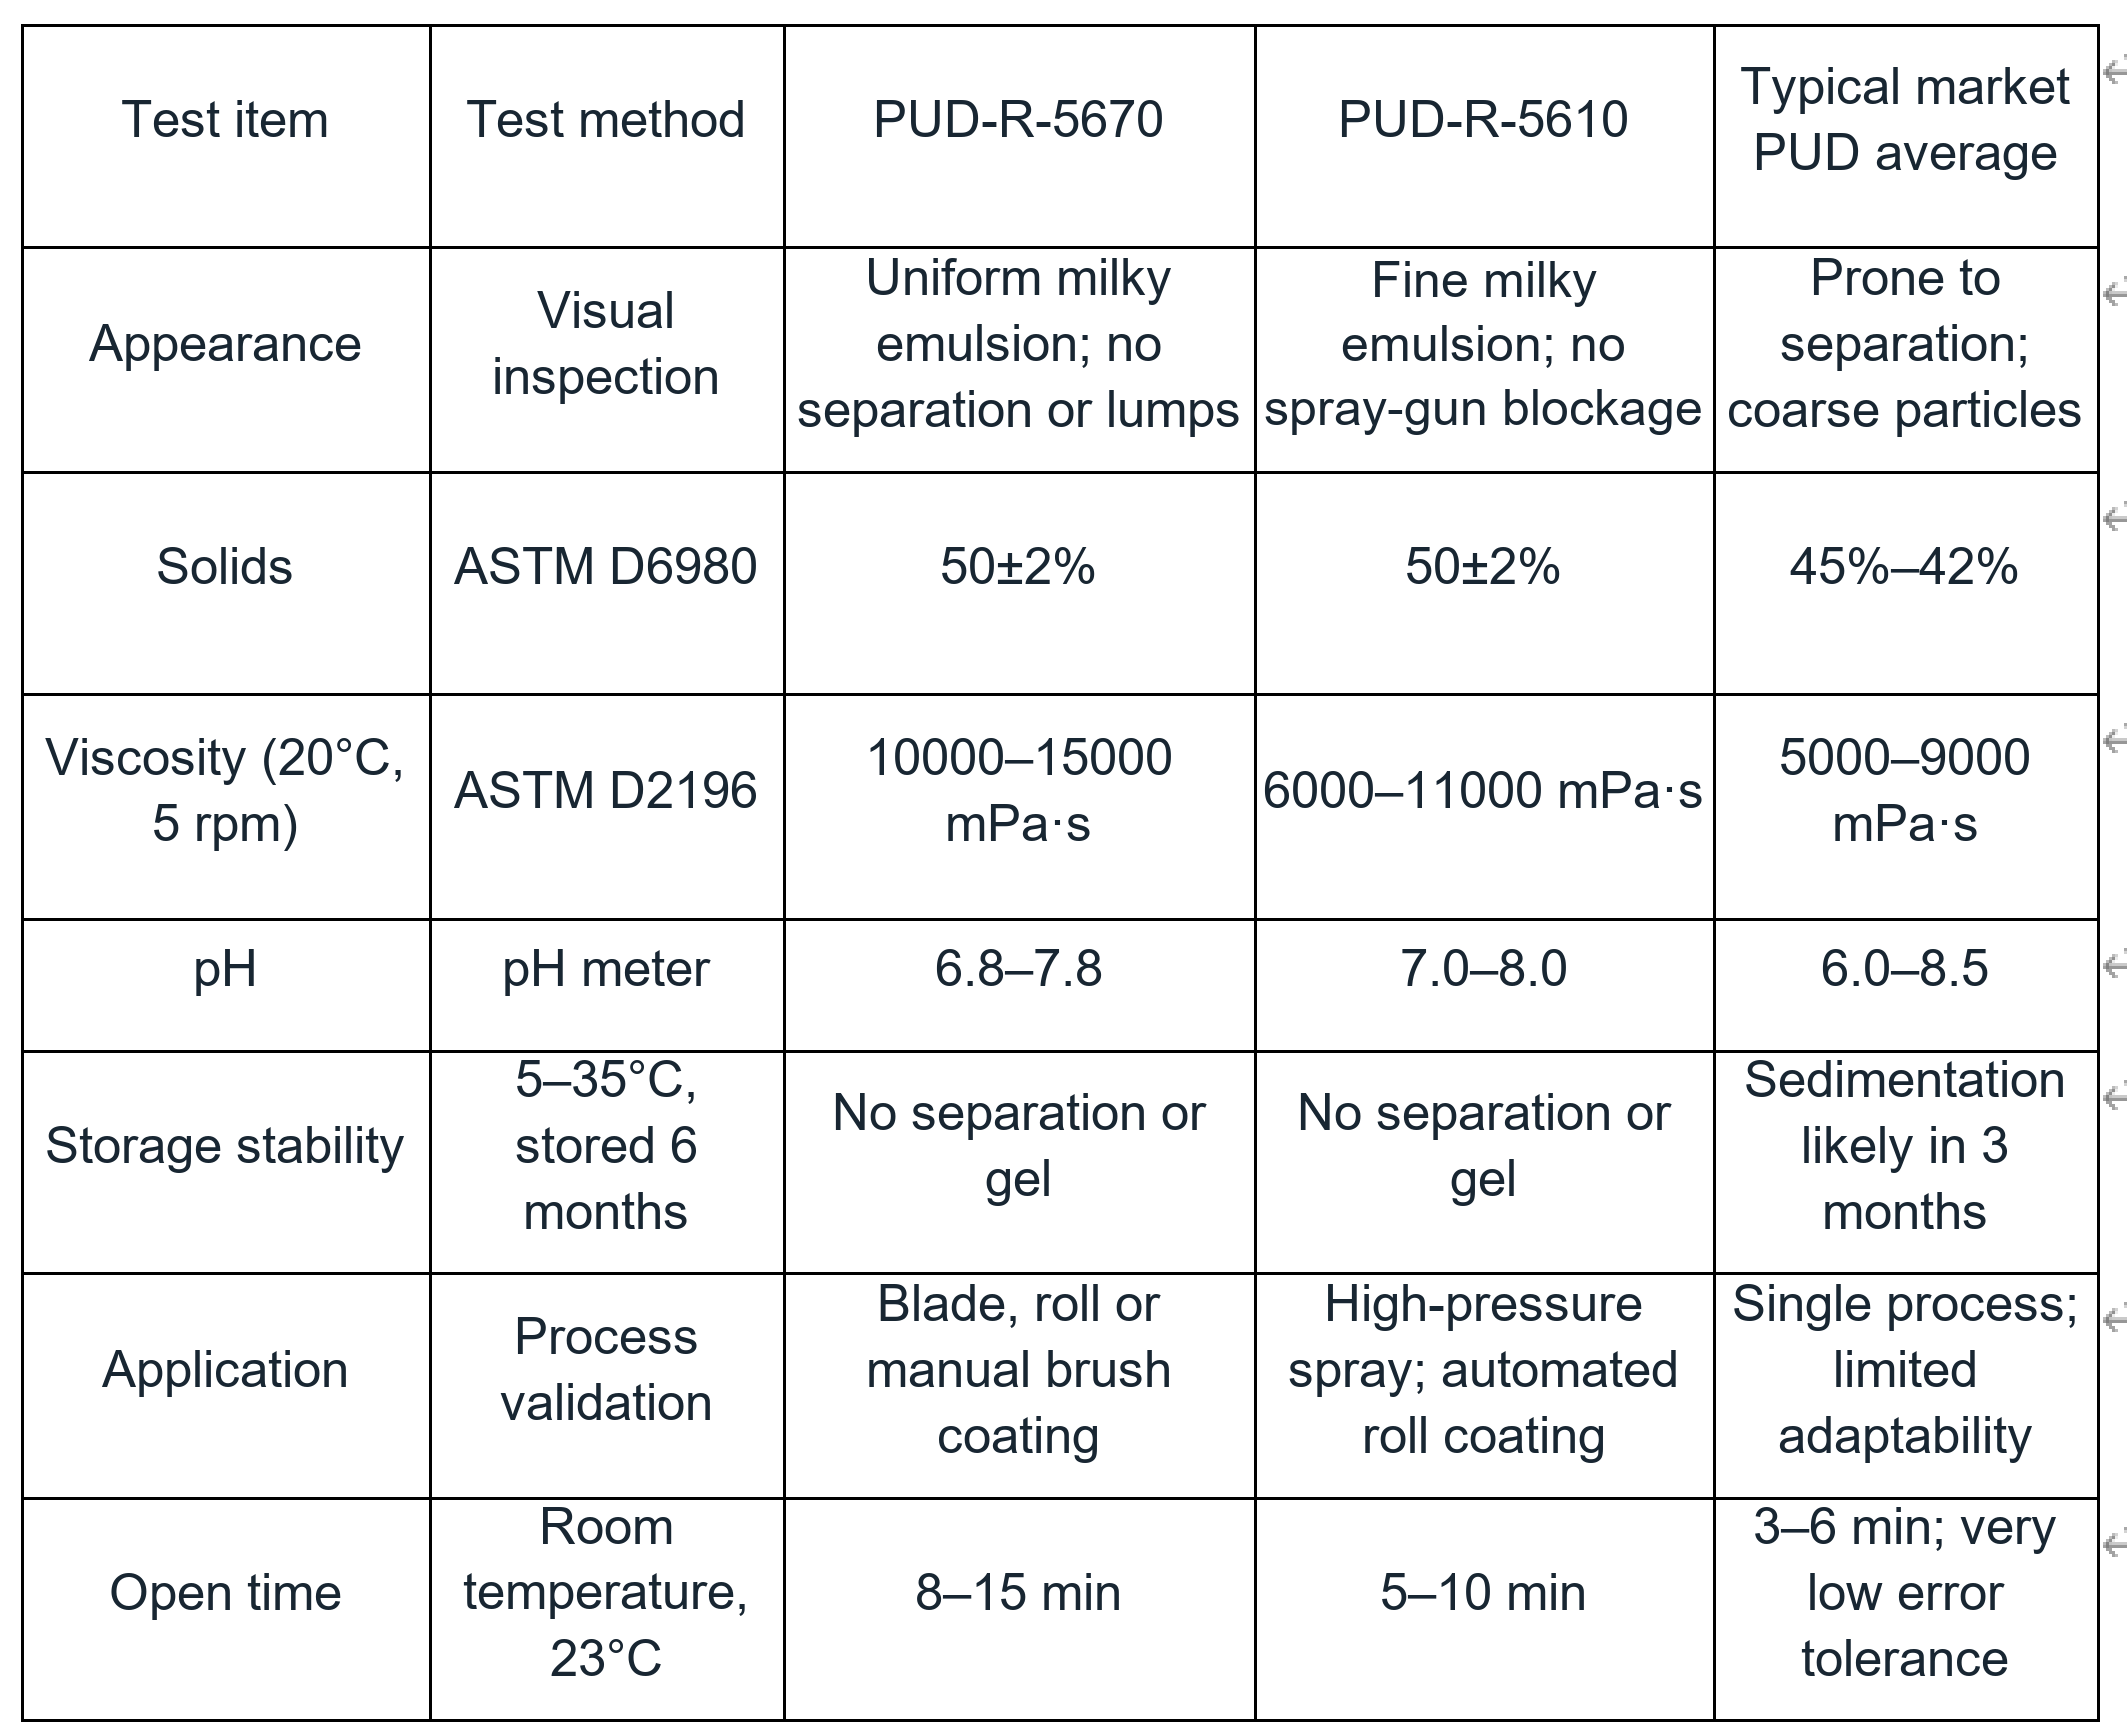
High solids are described as a core advantage. Compared with an ordinary market PUD, solids are stated to be more than five percentage points higher, allowing 20%-30% less adhesive for the same bonded area and reducing cost per interior set. Viscosity is tuned to the process: the manual grade is thick enough to resist sagging, while the line grade flows through a 2.0 mm spray setup during extended operation without blockage. An 8-15 minute open time gives operators freedom to reposition leather on complex surfaces and corners, reducing bubbles, wrinkles and rework.
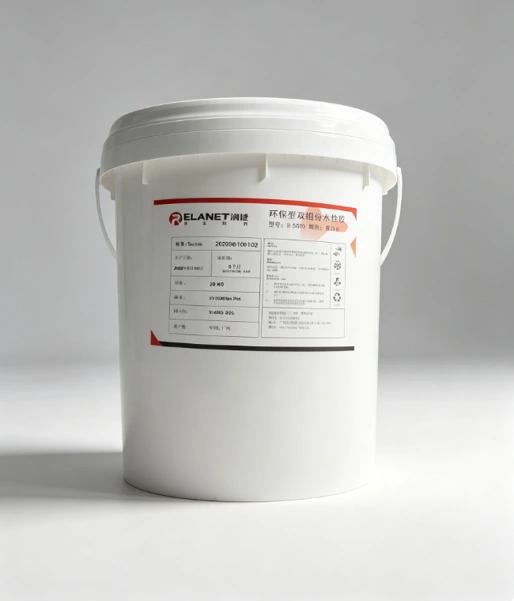
Original product-package photograph. The Chinese brand and physical label are retained as photographed; consult the current label and safety data sheet.
RELANET PUD finished-product packaging
(2) Mechanical bonding performance
Bond strength and film flexibility directly determine whether an interior component remains bonded and free of edge lift during long-term use. After curing, the two PUD products in the source manuscript exceeded the cited industry baseline in the following tests:
- Elongation at break and tensile toughness
Under ASTM D412, the source reports elongation at break of 600%-1,000% for RJ810 and 750%-1,100% for RJ830 at a 10°C workshop temperature. At 23°C, elongation exceeded 1,200%, with tensile strength of 28-32 MPa.
Conventional water-based PUDs are described as providing 300%-500% elongation at low temperature, increasing the risk of folded-edge cracking and corner lift during winter wrapping. The modified RELANET chain structure gives the film greater conformity, allowing it to deform with the skin during vibration and thermal expansion and contraction.
- 180° peel strength on multiple substrates
Peel force measured after 24 hours of curing:
- Microfiber leather + ABS carrier: ≥1,150 N/m.
- TPO skin + modified PP board: ≥980 N/m.
- Natural leather + EVA foam: ≥1,300 N/m.
- Flexible PVC skin + wood-plastic interior board: ≥1,050 N/m.
Skin failure during peel testing identifies the failure location of that specimen under those conditions. It does not establish equal strength on every substrate or pretreatment-free PUD bonding of PP and TPO. Validate cleaning, primer and activation requirements for the actual materials and adhesive; the confirmed PP process for R-7206 and R-7110 must not be applied to all PUD grades.
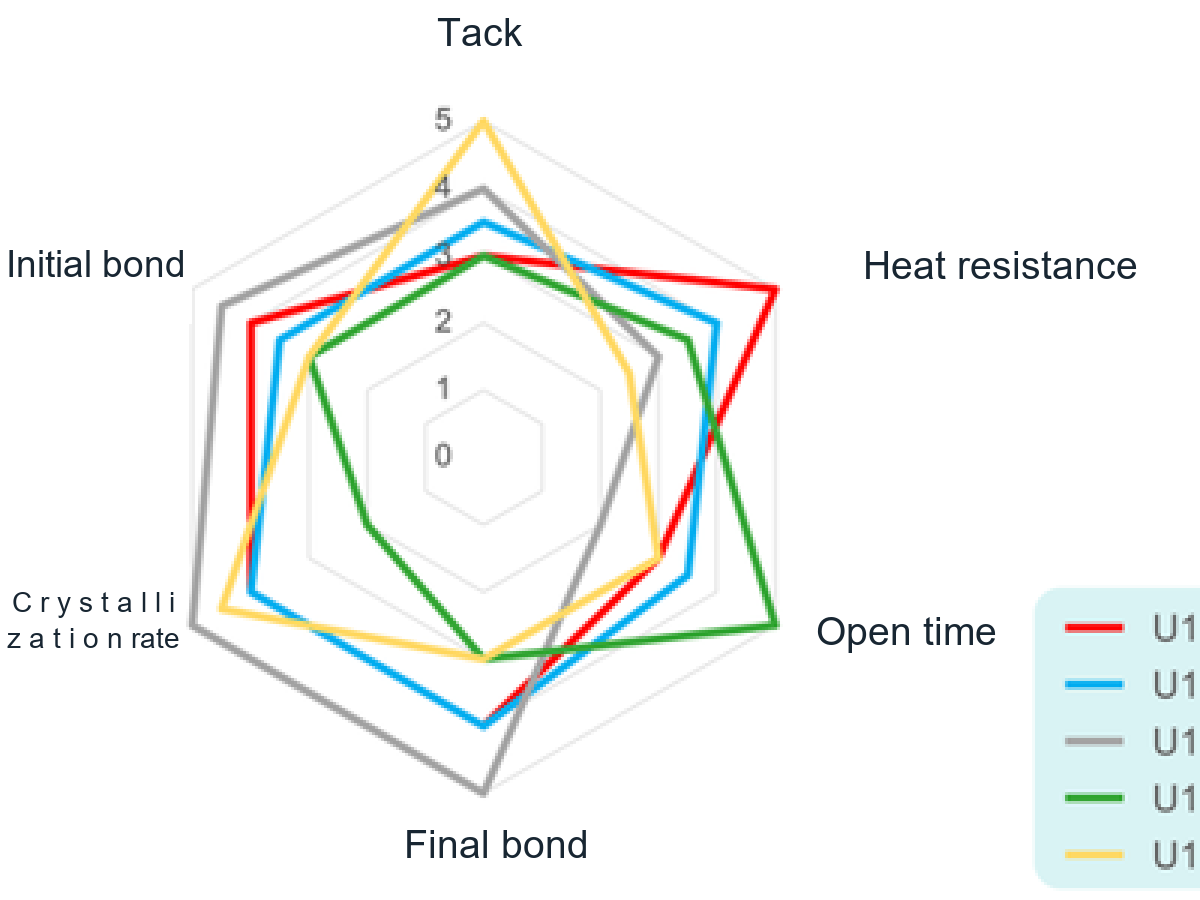
PUD bonding-performance radar comparison
- Creep resistance and vacuum-forming stability
In vacuum-forming tests at -0.09 to -0.1 MPa, the film continued to stretch without slipping or delaminating. The referenced line achieved saturated initial tack after 40-60 seconds of rapid activation at 120-130°C, within an activation window of 110-140°C. The source reports a 15%-25% increase in line efficiency and an end-of-line bonding defect rate below 0.3%, compared with an industry-average defect rate stated as 2%.
(3) Weathering and durability: vehicle-level environmental simulation
Automotive interiors may experience -40°C winter conditions, 90°C summer exposure, humid rainy seasons and long-term vibration. Adhesive durability affects a component's three-to-eight-year service life. The manuscript reports the following cyclic-aging results:
- High- and low-temperature cycling
After 50 cycles of four hours at -40°C followed by four hours at 90°C, peel-strength retention was ≥88%, without film whitening, embrittlement, shrinkage or debonding. The source states that ordinary market PUDs lost more than 40% of bond strength after 30 cycles and showed extensive corner lift.
- Humid-heat hydrolysis resistance
After 1,000 hours at 60°C and 95% RH, the film showed no hydrolysis or whitening and retained 85% of peel strength. Polycarbonate-modified chains improve hydrolysis resistance for hot, humid and coastal service and are intended to reduce moisture-related blistering and detachment.
- Heat exposure and yellowing resistance
The original material reports observations after 500 hours at 85°C. Verify the adhesive grade, bond-line thickness, specimen and original results before using them. An aliphatic structure can reduce yellowing tendency, but light leather and white TPO still require color-change and migration testing; permanent freedom from yellowing or skin contamination is not established.
- Resistance to oils and cleaners
After 72-hour contact with hand cream, leather-care product and interior cleaner, the source reports no significant bond-strength loss and no swelling of the adhesive layer, addressing a common after-sales failure caused by interior cleaning.
(4) Separate odor, VOC and regulatory assessment
As new-energy vehicle manufacturers tighten odor and VOC controls, RELANET addresses environmental performance from the raw-material stage:
- A VOC result must identify its specimen, method, unit and acceptance criterion. The original values of below 8 mg/L and 50 mg/L lack a directly comparable test basis and must not be presented as a GB/T 27630 adhesive limit or compliance result. Agree the component VOC test and target for the project.
- Evaluate odor using the customer-specified NES M0160 revision, sample and conditions; any grade requires a corresponding report. Odor testing does not replace occupational-exposure, ventilation or fire-protection assessment and cannot justify removing production safeguards.
- The cured adhesive and complete laminate still require project-specific emission testing, with individual targets such as acetaldehyde, toluene and xylene checked separately. Component results cannot establish complete-vehicle air-quality compliance or an absence of emissions from every cured grade.
- The water-based system is described as outside hazardous-chemical classification for the stated product, reducing storage, transport and hazardous-waste costs relative to solvent-borne adhesive and lowering safety-management pressure.
Finished appearance of an environmentally oriented interior application
(5) Process compatibility advantages
For initial process planning, the original material lists manual open time of 8–15 minutes, line open time of 5–10 minutes, tack-free drying of 10–25 minutes at room temperature and oven drying of 3–8 minutes at 80°C. Reconfirm these windows for the grade, coat weight, humidity and equipment. Different coating and forming processes may require different formulations. Determine cleaning, primer or activation separately for PUD bonding of PP and TPO; the confirmed PP capability of R-7206 and R-7110 is not a PUD property. Calculate rework, material and cycle-time effects from controlled line records rather than promising fixed savings.
(6) Main application scenarios
Instrument and door-panel wrapping requires evaluation of the skin, backing, carrier and folded-edge loads. Seats and armrests add repeated compression and abrasion; headliners and luggage boards require control of absorption, warpage and humid-heat durability. Enclosed recreational-vehicle cabins still require odor and VOC assessment. Select PUD adhesives through combined material, process, appearance and durability validation. One formulation does not automatically cover every part, and a water-based system does not establish vehicle compliance or fixed savings.
Separate odor, VOC and durability validation
NES M0160 addresses odor testing of automotive interior parts. It does not replace VOC, vehicle-cabin air-quality, durability or regulatory assessment. Confirm the revision, sample, conditions and targets for the customer project; naming a standard does not establish a pass.
- Use the customer-specified NES M0160 revision and odor test conditions. Any stated grade requires a valid report for the corresponding sample.
- Confirm VOC methods and targets separately; Nissan projects may involve NES M0402 and NES M0403. GB/T 27630 concerns passenger-vehicle cabin air quality and is not a single adhesive VOC limit. Check REACH, ELV and durability requirements separately.
Sources and validation basis Nissan · NES M0160 / NES M0402 / NES M0403